 Philadelphia, PA
 Atlanta, GA
 Chicago, IL
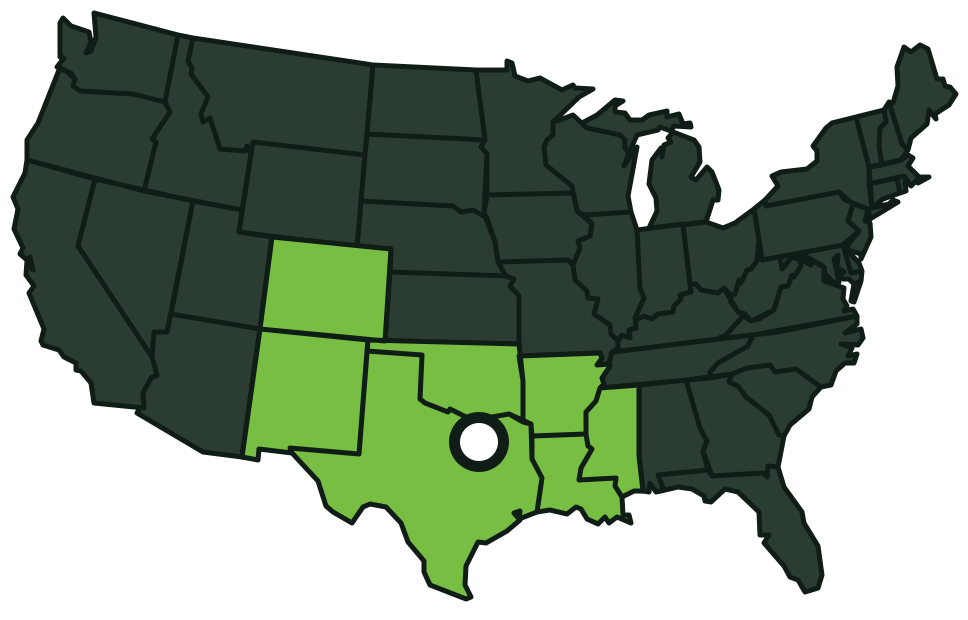 Dallas, TX
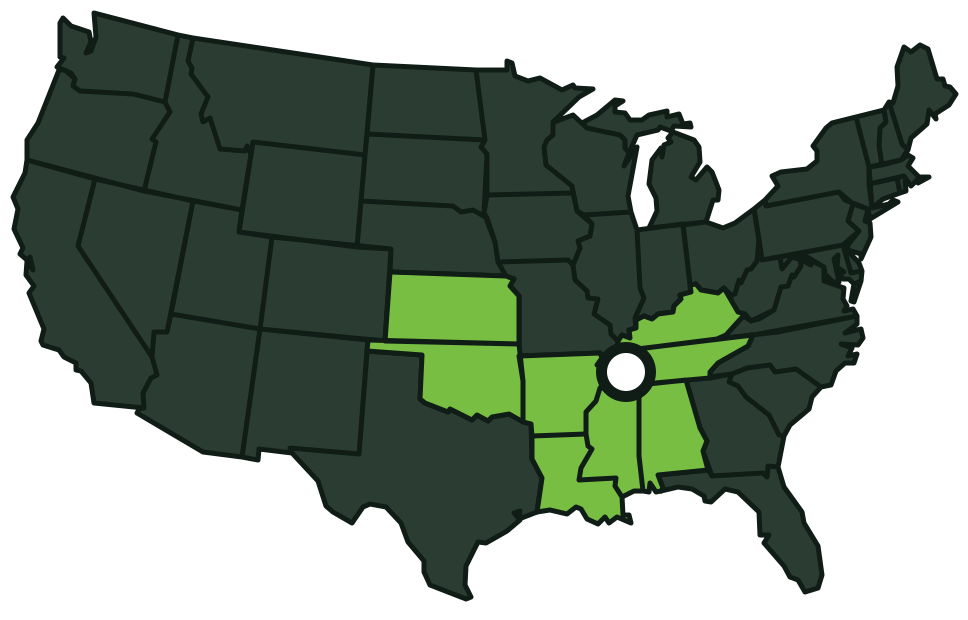 Jackson, TN
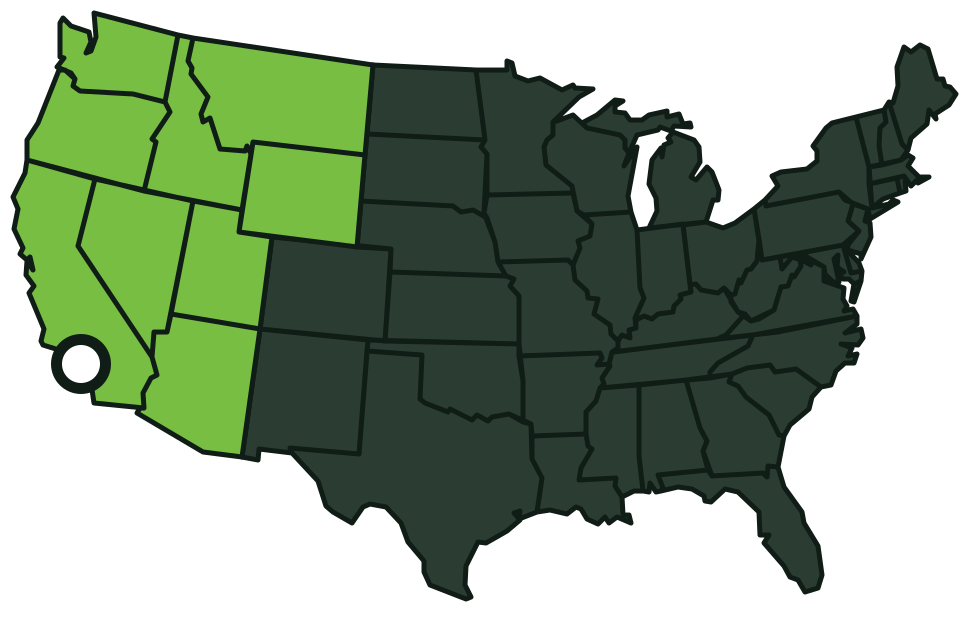 Los Angeles, CA
Selecting the Right Shield: A Guide to Protective Coatings for Harsh Industrial Environments
Learn how to select the right protective coating system for your harsh industrial environment and maximize asset service life.
Not all industrial coatings are created equal - and in a demanding industrial environment, choosing the wrong one is just as costly as skipping the coating altogether. The coating chemistry you specify determines how well your assets resist corrosion, chemical attack, UV degradation, abrasion, and thermal stress. Get it right and you are looking at 15 to 25 years of protection. Get it wrong and you are looking at premature failure, accelerated corrosion, and the full cost of recoating on a compressed timeline.
This guide breaks down the most widely used protective coating types for harsh industrial environments, what each one does well, where each one falls short, and how to match the right system to your specific exposure conditions.
Why Coating Chemistry Matters More Than Brand
Before diving into specific coating types, it is worth understanding why chemistry - not brand, not price point, not color - is the primary selection criterion for industrial protective coatings.
Industrial environments subject coatings to stresses that simply do not exist in commercial or residential applications: immersion in chemicals, constant UV exposure, thermal cycling between extremes, mechanical abrasion from traffic and equipment, and aggressive atmospheric corrosion in coastal, chemical, or high-humidity zones. Each of these stressors degrades coatings through different mechanisms. A coating formulated for UV stability may have poor chemical resistance. A coating with outstanding chemical resistance may chalk and fade rapidly outdoors. Matching chemistry to environment is what determines service life.
This selection process always begins with thorough surface preparation - because even the most perfectly specified coating will fail prematurely on an improperly prepared substrate. Chemistry and surface prep are inseparable.
The Core Industrial Protective Coating Types
Epoxy Coatings: The Industrial Workhorse
Epoxy coatings are the most widely specified coating in industrial applications for good reason. Two-component epoxy systems - resin plus hardener - cure through a chemical reaction that produces a thermoset film with outstanding adhesion, hardness, and moisture barrier performance. They resist a broad spectrum of chemicals including solvents, acids, and alkalis, and they provide excellent protection against corrosion when applied over properly prepared steel.
Best applications: Structural steel, manufacturing equipment, tanks, concrete floors, chemical processing environments, and any interior application requiring hard-wearing chemical resistance.
Limitation to know: Epoxies chalk and lose gloss when exposed to UV - a process called chalking. For exterior applications, epoxy is almost always used as a primer or intermediate coat, with a UV-stable topcoat applied over it.
Polyurethane Coatings: UV Stability and Finish Quality
Where epoxy fails outdoors, polyurethane excels. Polyurethane topcoats - particularly aliphatic polyurethanes - deliver exceptional UV stability, color retention, and gloss maintenance over years of outdoor exposure. They are also tougher and more abrasion-resistant than epoxy, making them the default topcoat choice for exterior structural steel, bridges, heavy equipment, and any application where long-term appearance matters alongside protection.
Two-component polyurethane systems are specified for the most demanding exterior industrial facility painting projects. They are typically applied over a zinc-rich primer and epoxy intermediate coat - a three-coat system that addresses adhesion, corrosion protection, barrier performance, and UV resistance in a single coordinated specification.
Best applications: Exterior structural steel, bridges, manufacturing facility exteriors, heavy equipment, and architectural industrial surfaces requiring long-term gloss and color retention.
Zinc-Rich Coatings: Sacrificial Protection for Steel
Zinc-rich primers operate on a fundamentally different principle than barrier coatings. Rather than simply keeping moisture and oxygen away from the steel, zinc-rich coatings provide galvanic - or sacrificial - protection. The zinc corrodes preferentially, protecting the underlying steel even if the coating film is scratched or damaged. This is the same principle behind hot-dip galvanizing, delivered in a coating system.
Inorganic zinc silicate coatings are the highest-performance option in this category, offering excellent resistance to elevated temperatures and aggressive atmospheric corrosion. They are widely specified in offshore, petrochemical, and marine environments where ISO 12944 C5 and CX corrosivity classifications demand maximum protection.
Best applications: Marine and offshore structures, petrochemical facilities, bridges, coastal infrastructure, and any steel in highly aggressive corrosive environments. As we covered in our complete guide to industrial painting and protective coatings, zinc-rich primers are almost universally specified as the first coat in high-performance multi-coat systems for steel in C4 and above environments.
High-Temperature Coatings: When Heat Is the Enemy
Standard coating chemistries break down under sustained heat. Silicone-based and inorganic coatings formulated for elevated temperature service can withstand continuous exposure in ranges where conventional epoxies and urethanes would crack, discolor, and disbond. These coatings are engineered for thermal cycling - the repeated expansion and contraction that destroys coatings that lack sufficient flexibility at elevated temperatures.
For facilities with boilers, furnaces, exhaust stacks, and high-heat process piping, specialized high-temperature boiler painting and coating services require a completely different product selection approach than the rest of the facility. Applying a standard industrial epoxy to a boiler surface is not just ineffective - it will fail rapidly and potentially create a maintenance hazard.
Best applications: Boilers, exhaust systems, chimneys, furnaces, high-heat process equipment, and any surface that routinely exceeds 200°F in service.
Polysiloxane Coatings: Premium Performance, Extended Service Life
Polysiloxane coatings represent the premium tier of industrial topcoat technology. They deliver weathering resistance, UV stability, and chemical resistance that outperforms conventional polyurethanes - often significantly extending the recoating interval compared to standard systems. The tradeoff is cost: polysiloxanes carry a higher per-gallon price. But when that higher upfront cost is evaluated against the total lifecycle cost of a coating system - including future maintenance painting, surface preparation, and downtime - polysiloxanes frequently deliver a lower cost per year of protection.
Best applications: Bridges, large tanks, offshore structures, and any project where extended recoating intervals and reduced lifecycle maintenance costs are the primary objectives.
Elastomeric and Roof Coating Systems: Flexible Protection at Scale
For large industrial roof surfaces facing UV exposure, thermal cycling, ponding water, and in some facilities, chemical fume exposure, elastomeric and specialized roof coating systems provide a different kind of protection than structural coating systems. These formulations are engineered to flex with the substrate through thermal movement cycles without cracking, bridging seams and fasteners that would otherwise be leak points.
Industrial roof coating systems - including acrylic, silicone, and polyurethane roof coatings - can add 10 to 20 years of service life to aging metal and low-slope roofs, representing a significantly better economic outcome than premature full roof replacement.
Matching Coating to Environment: The ISO 12944 Framework
Specifying the right protective coating system is not guesswork - it follows the ISO 12944 corrosivity classification framework, which categorizes environments from C1 (very low corrosivity, heated interiors) through C5 (very high, aggressive industrial or coastal atmospheres) and CX (extreme, offshore). Each category carries defined requirements for coating system performance and dry film thickness.
A manufacturing plant interior might qualify as C2 or C3. A coastal petrochemical facility is C5. An offshore platform is CX. The jump from C3 to C5 is not just a more aggressive coating - it is typically a more rigorous surface preparation standard, additional coat layers, and greater total dry film thickness. Understanding where your assets sit on this scale is the starting point for every coating specification. As part of a comprehensive industrial painting and coatings strategy, ISO 12944 classification should inform every major coating decision you make.
The Bottom Line on Coating Selection
The right protective coating for a harsh industrial environment is never the cheapest option, and it is rarely the most expensive one either. It is the coating chemistry that most precisely matches the specific corrosion mechanisms, chemical exposures, temperature range, and UV conditions your assets actually face - applied over a properly prepared surface by a contractor who understands the difference.
Getting that specification right is what separates a coating system that performs for decades from one that becomes a recurring maintenance problem. Contact the Kelly Industrial Services team to discuss your facility’s specific exposure environment and build a coating specification designed to last.
Industrial painting and coatings
How Scheduled Industrial Painting Reduces Maintenance Costs and Extends Asset Life
Learn how a scheduled industrial painting program reduces maintenance costs, prevents corrosion failures, and extends the life of your critical assets.
Read moreSelecting Industrial-Grade Finishes: Interior and Exterior Coatings for Facility Durability
Learn how to choose durable interior wall coatings, prepare concrete walls for industrial paint, and select long-lasting exterior building finishes.
Read moreThe Complete Guide to Industrial Painting: Surface Preparation, Protective Coatings, and Long-Term Asset Protection
Learn how industrial painting protects structures, equipment, and facilities. Explore surface prep, coating systems, and long-term protection strategies.
Read moreTell us about the facility.
We'll tell you straight.
A specialist reviews every request, not a call center. If it is not Kelly work, we will say so and point you in the right direction.